Trinity NDT WeldSolutions Private Limited

NADCAP Aerospace Trinity NDT India

NDT Certification Courses

Phased array PAUT equipment calibration

PAUT vs Conventional UT — Which Ultrasonic Testing Method Do You Need?

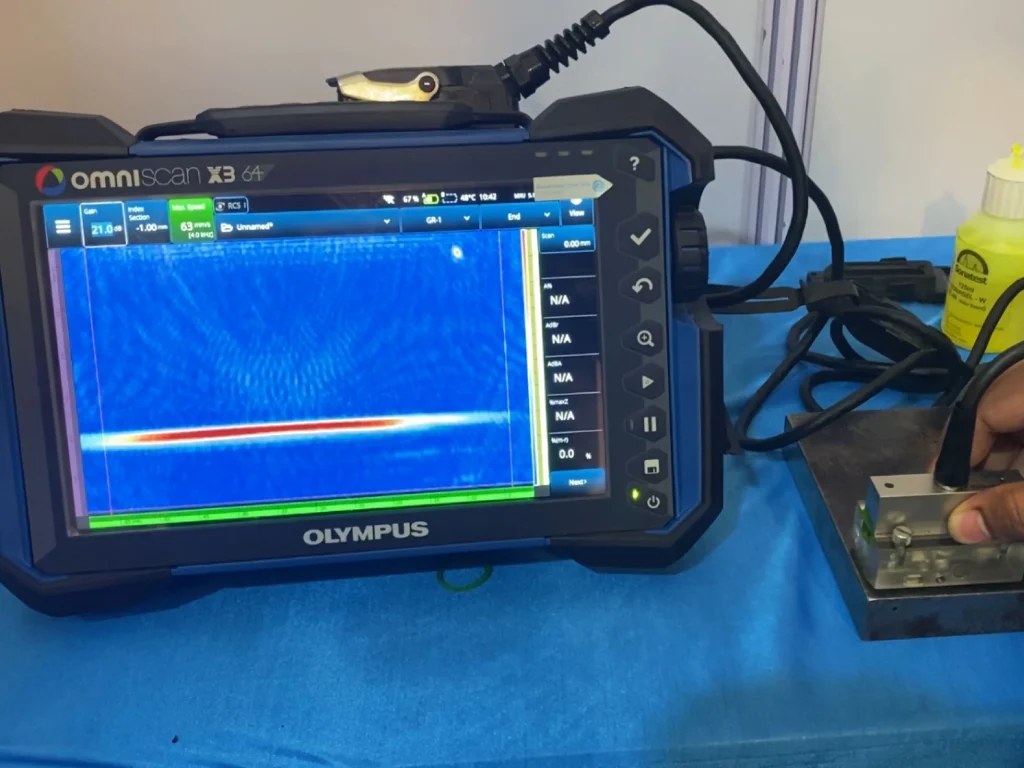
PAUT vs Conventional UT: When Do You Actually Need Phased Array? Here’s a conversation we have almost every week: a client calls asking for “PAUT testing” on a job, and after a few questions it turns out conventional ultrasonic testing would have done the job perfectly well — for a fraction of the cost and

PAUT vs Conventional UT — Which Ultrasonic Testing Method Do You Need? Read More »
Radiography Testing Industrial RT X-ray – FAQ

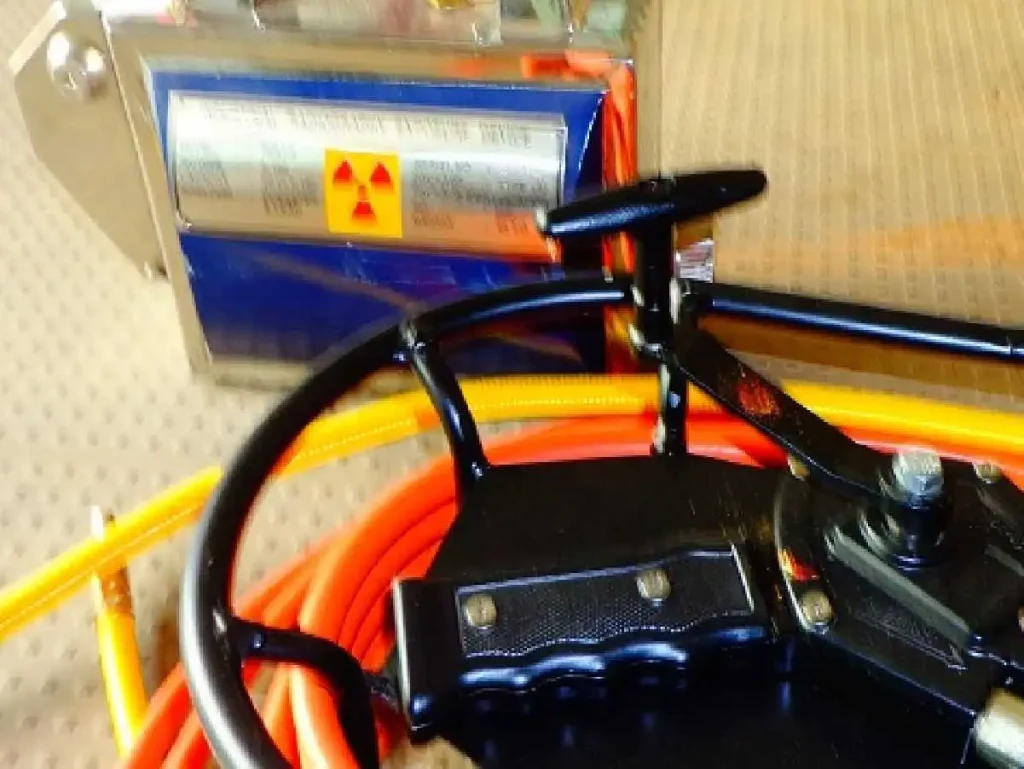
What kind of flaws will Radiography testing detect? Objective of Radiography Testing is to detect internal flaws. Volumetric flaws such as voids, pinholes, slag, shrinkage are easily detected, whereas, planar defects such as laminations, laps and seams are difficult to defect. A defect should create notable amount of sectional difference to get detected. Flaws whose

Radiography Testing Industrial RT X-ray – FAQ Read More »

Guide for Industrial Radiography Artifacts

Guide for Industrial Radiography Artefacts All indications appearing in a radiograph are to be interpreted. Interpretation requires analysing the indication as to whether it is a true indication due to discontinuities or a false indication due to problems with film manufacturing, mishandling of film or poor storage. The interpreter should be able to distinguish a

Guide for Industrial Radiography Artifacts Read More »

Guide for Industrial Radiography Artifacts

Guide for Industrial Radiography Artifacts All indications appearing in a radiograph are to be interpreted. Interpretation requires analysing the indication as to whether it is a true indication due to discontinuities or a false indication due to problems with film manufacturing, mishandling of film or poor storage. The interpreter should be able to distinguish a

Guide for Industrial Radiography Artifacts Read More »

Weld Repairs during Production and In-service Maintenance

Weld Repairs during Production and In-service Maintenance – Overview Types of Weld Repairs Weld repairs can be divided into two specific areas:1 Production2 In-service Reasons For Weld Repair The reasons for making a repair are many and varied, from the removal of weld defects induced during manufacture to a quick and temporary running repair to

Weld Repairs during Production and In-service Maintenance Read More »

ISO3834 Quality Management in Welding Companies

Quality Management in Welding – ISO3834 Certification Requirements Basic Standard for QMS    ISO 9001 -2000 Manufacturing    ISO 3834, EN 1011, ISO 5817 Personnel    ISO 9606, EN 287, ISO 14731, ISO 14732 Procedures    ISO 15607 – 15614 Testing and Inspection Personnel    ISO 9712, EN 1289 Basis for ISO 3834  series of

ISO3834 Quality Management in Welding Companies Read More »

How to Do Magnetic Particle Testing as per ASTM E709 & E1444

Introduction Magnetic Particle testing is also known as MPI or MPT is a well accepted NDT method to reveal surface and below surface flaws. Applied for ferro-magnetic metals such as Iron, Nickel and Cobalt alloys. Due to its effectiveness in detecting flaws, industries such as Automobile, Oil and Gas, Processing and Aerospace accepted as a

How to Do Magnetic Particle Testing as per ASTM E709 & E1444 Read More »

How to Do Magnetic Particle Testing as per ASTM E709 & E1444

Introduction Magnetic Particle testing is also known as MPI or MPT is a well accepted NDT method to reveal surface and below surface flaws. Applied for ferro-magnetic metals such as Iron, Nickel and Cobalt alloys. Due to its effectiveness in detecting flaws, industries such as Automobile, Oil and Gas, Processing and Aerospace accepted as a

How to Do Magnetic Particle Testing as per ASTM E709 & E1444 Read More »